Conveying and sortation for live fulfillment

Intralox conveyor systems planned for rate you can accept

Translate carton, tote and pallet geometry, SKU mix, peak-window demand, accumulation and divert rules into a conveying and sortation concept that maintenance and controls teams can hand over with evidence.

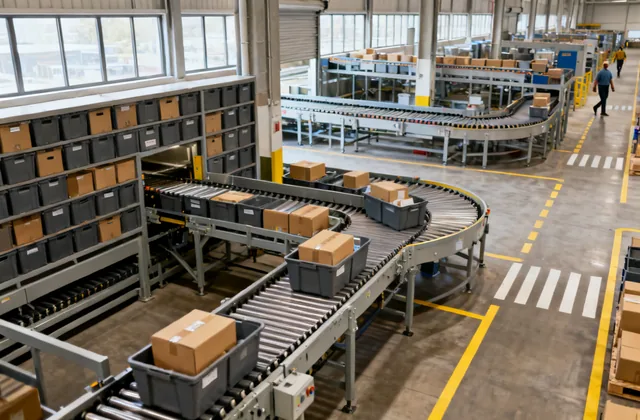
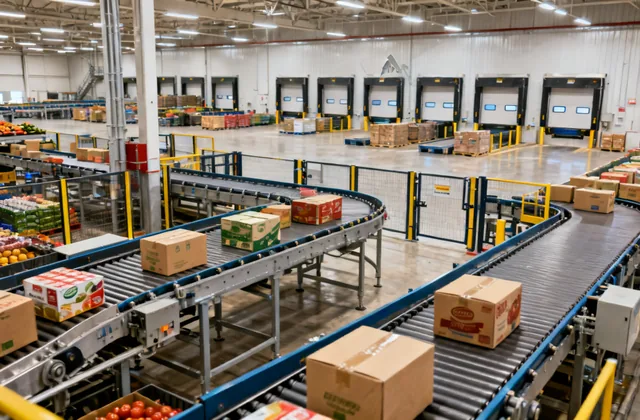
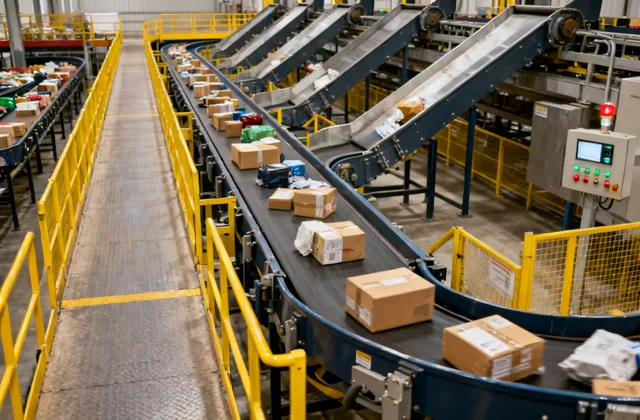
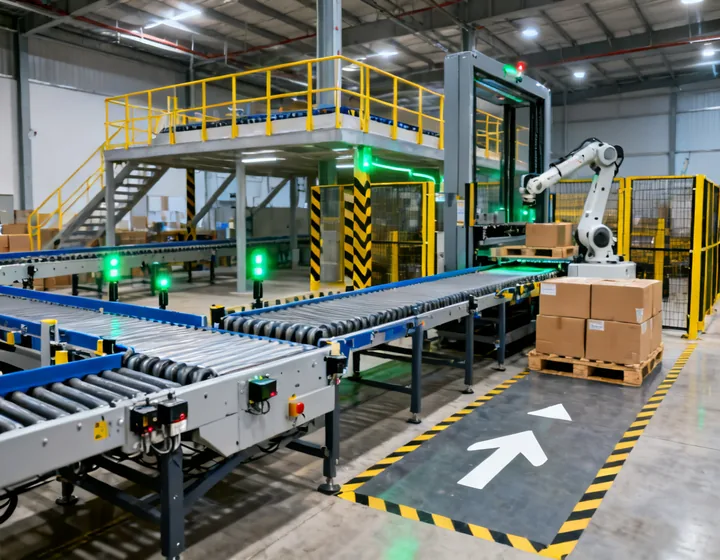
Distribution center conveyor and sortation mezzanine in operation
Load unitCarton, tote or pallet envelope recorded
SKU / order mixVelocity bands and line structure stated
Peak windowAccumulation and divert demand included
RecoveryJam, divert fail and restart path documented
Conveying, sortation and palletizing scope

Start with the featured flow cell, then compare supporting modules

Intralox organizes the portfolio around the interfaces that decide whether a stated rate survives peak windows: belt conveying, activated-roller divert, spiral elevation and palletizing handoff.

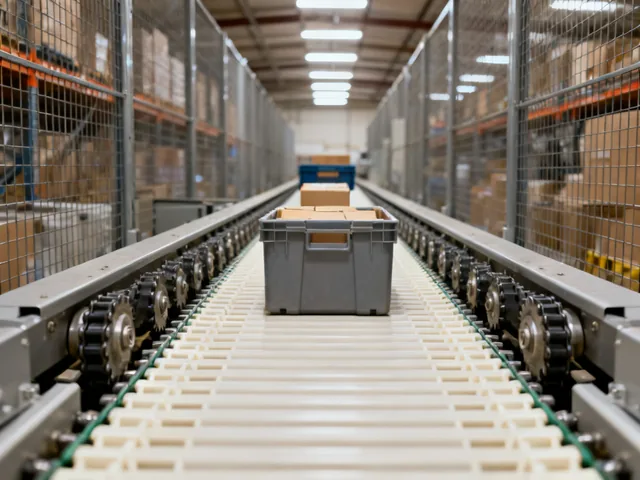
Modular plastic belt conveyor line

Modular belt conveyors

Belt selection follows product friction, incline, washdown and access for pin removal and sprocket inspection.

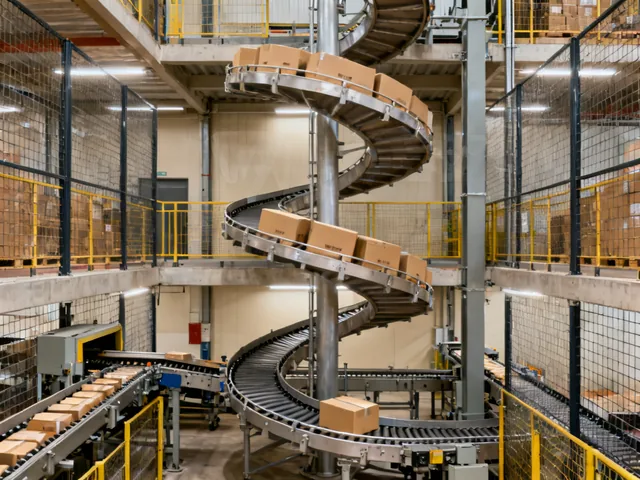
Spiral conveyor elevating cartons between levels

Spiral elevation

Elevation modules connect levels without hiding the buffer and recovery consequences at infeed and discharge.

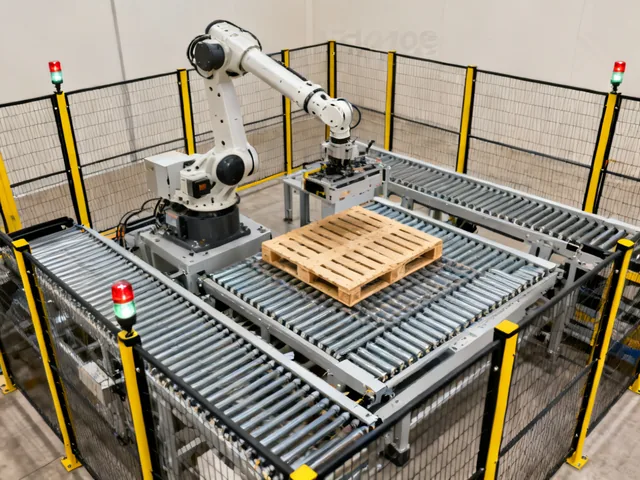
Robotic palletizing cell fed by conveyor

Palletizing interfaces

Case presentation, pattern integrity and rejected-load disposition are specified before a robotic or conventional cell is quoted.

Operating profiles

Three fulfillment environments, three different divert boundaries

E-commerce fulfillment conveyor and sorter

E-commerce fulfillment

Campaign peaks make gap control, recirculation and reject handling as important as the nominal sorter rate.

Grocery distribution case conveyor lines

Grocery distribution

Wave departures, mixed case friction and temperature transitions change belt selection and buffer sizing.

Parcel sortation hub conveyor network

Parcel & hub sortation

Irregular parcels stress divert confirmation, chute capacity and the restart sequence after a jam.

Review Operating Profiles
Decision checkpoints

Keep rate, buffers and acceptance evidence in the same conversation

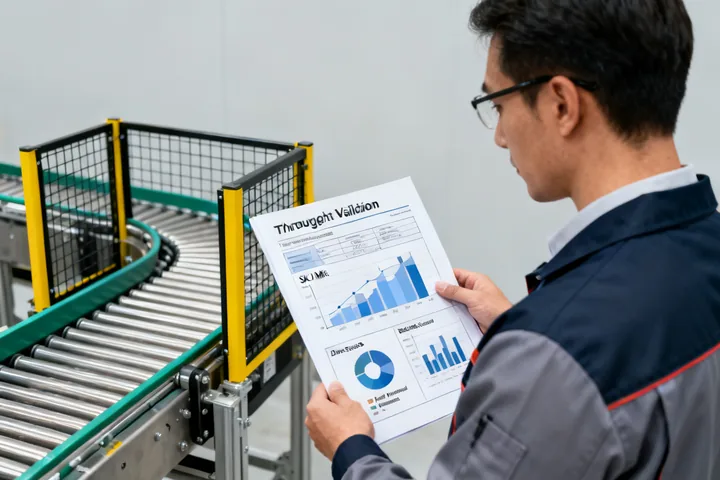
Throughput validation worksheet beside conveyor line
Throughput validation

A rate claim without mix and buffers is incomplete

Validate design rate against SKU mix, order profile, peak window, accumulation, replenishment and exception recovery. Intralox records the induction method, gap strategy and what happens when a downstream zone stops accepting product.

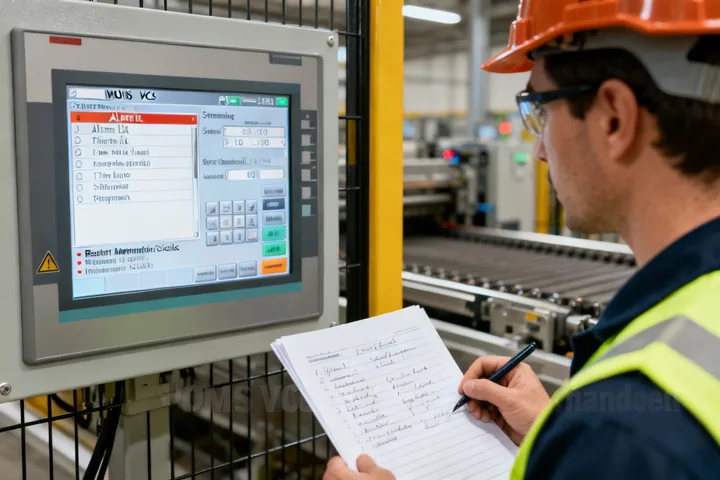
Controls responsibility review at conveyor HMI
Controls responsibility

Document who owns command, timeout and restart

WMS, WCS, WES, PLC and fleet-management ownership must be visible before interface definitions freeze. FAT scripts exercise handshakes; SAT confirms installed geometry, safety devices and recovery scenarios with real loads.

Bring the flow data before the layout drawing

A useful first review can begin with load envelopes, peak windows, divert destinations and a marked building plan showing elevation changes.

  • Carton, tote or pallet dimensions and mass bands
  • Daily and peak induction windows
  • Divert, merge and recirculation rules
  • WMS/WCS/PLC ownership and acceptance questions

Start the conveyor brief